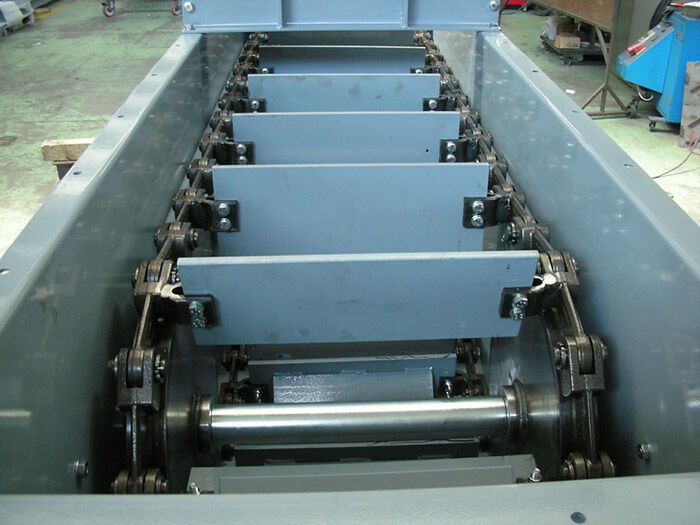
Key Features:
– Fully Enclosed & Dust-Controlled Design
– Horizontal & Inclined Conveying
– Forged, Roller & Heavy-Duty Chain Options
– Capacity Up to 200 TPH
– Conveyor Length Up to 60 m per Section
– MS, SS304 & SS316 Construction
– AR400 & UHMWPE Wear Liners
– Geared Motor with VFD & PLC Options
– Custom Engineered for Specific Materials
Applications:
Drag chain conveyors are designed for handling fly ash, coal, cement clinker, limestone dust, wood chips, rice husk, biomass, bagasse, grain, fertilizer, and mineral powders. The enclosed trough helps reduce material spillage and dust during transportation, making them suitable for demanding industrial environments.
With 18+ years of manufacturing experience and 1,000+ conveyor installations, Neo Conveyors provides application-specific drag chain conveyor systems with in-house engineering, fabrication, installation, and service support across India.